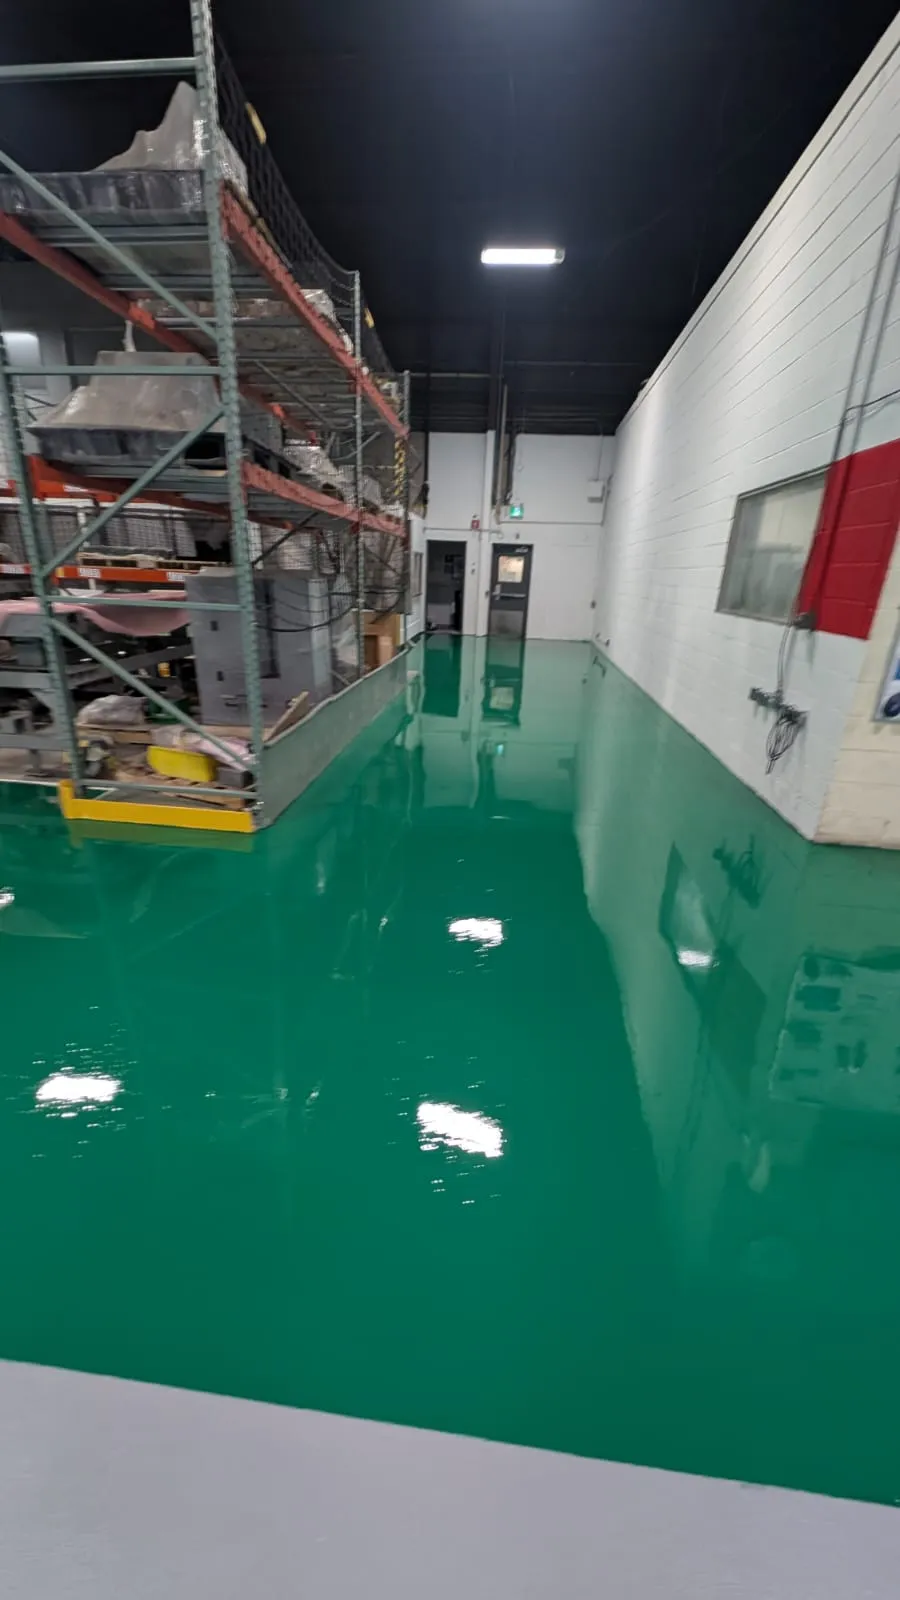
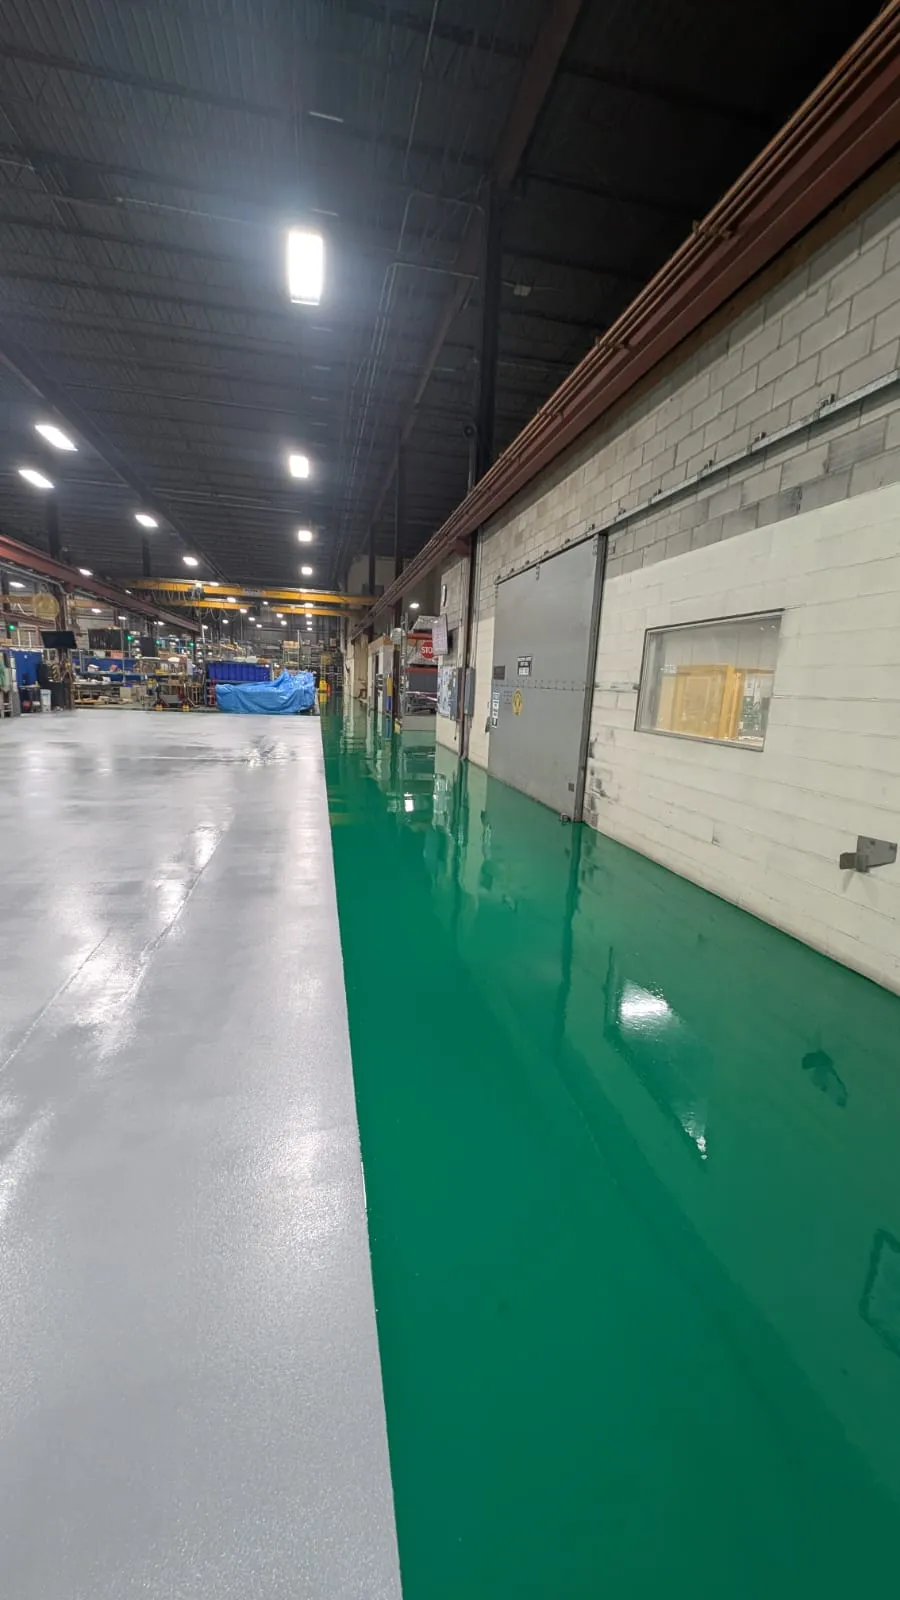
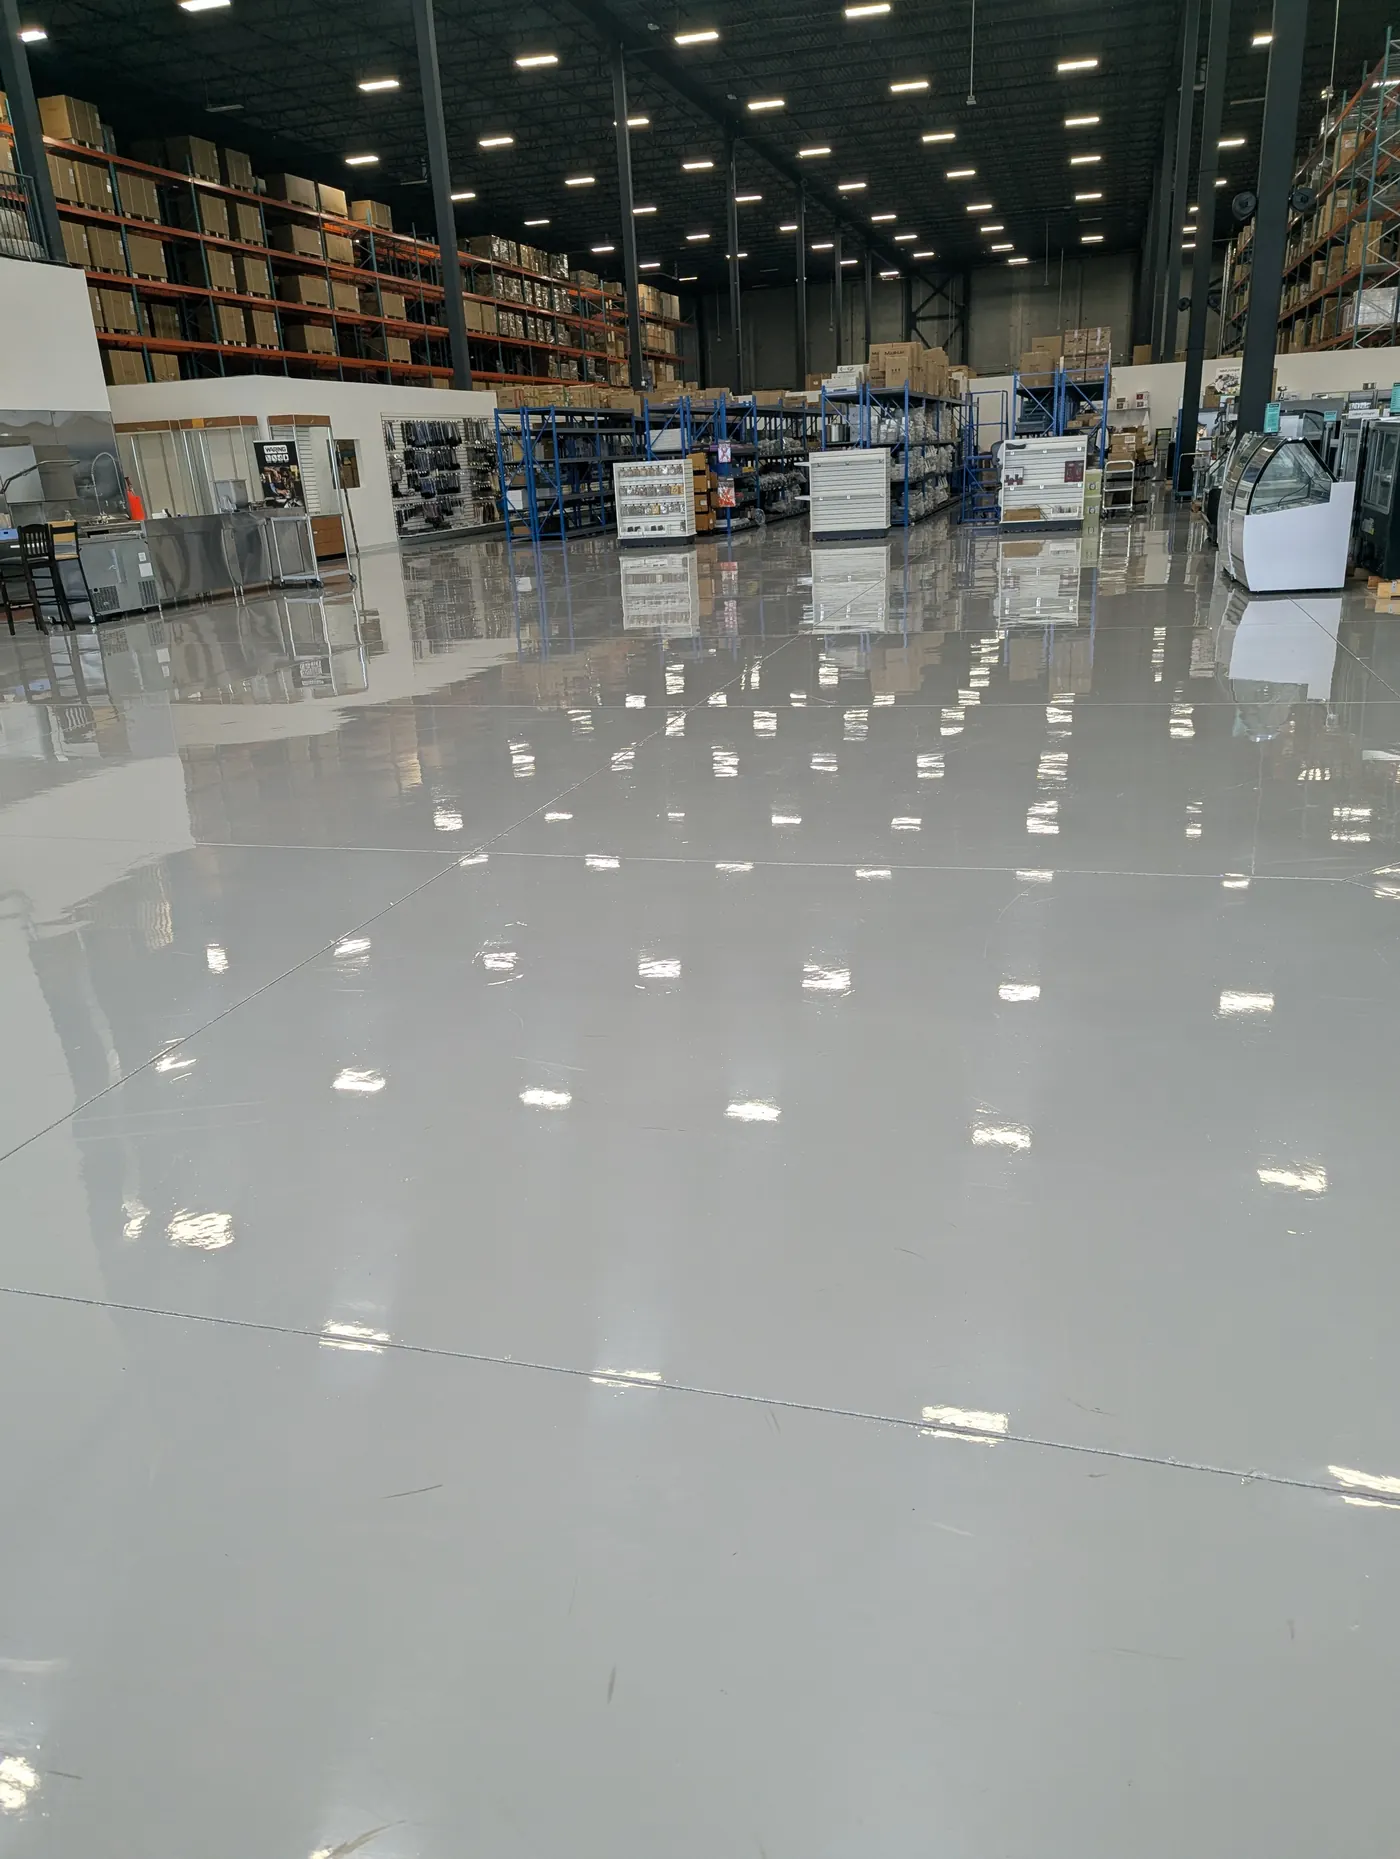
Chemical, impact and thermal resistant systems for Milton manufacturing plants, machine shops, metal fabricators and process facilities. Specified against what actually lands on your floor, not against a generic brochure.
Free on-site assessment, usually within the week. Milton is a short drive from our Burlington base. Written scope, fixed price, no obligation.
Plant floors do not send you an invoice. They just show up as housekeeping hours, maintenance costs and, eventually, a repair that has to happen during production.
Etched, softened or discoloured concrete has lost its top layer. That layer does not grow back, and the next spill goes deeper than the last one.
Porous, contaminated concrete holds oil and coolant no matter how often it is cleaned. That is a labour cost with no end date attached to it.
A system laid over a shake-on hardener, over slab moisture or over contamination lets go inside two years. Removing the failed coating then costs more than proper preparation would have in the first place.
Traffic segregation, contamination control and housekeeping all get scored, and the floor is the visible evidence for all three.
Milton's plants run heavy, from a Magna stamping operation to stone wool and electrical manufacturing, and the failure we see is a thin coating specified for a lighter shop. Thickness is the fix, and it goes in the written scope so you can compare it against the other quote.
The expensive floor is the one you end up doing twice.
Advanced manufacturing supports more than 6,500 jobs in Milton according to the Town's 2025 report. Karmax Heavy Stamping, a Magna stamping plant, is on Market Drive, and Rockwool, Eaton, 3M and Schneider Electric are all named by InvestMilton across the 401 Business Park and Derry Green. Heavy stamping, stone wool and electrical manufacturing mean impact, hot debris, oil and constant forklift traffic, which is a different floor from a light assembly shop. In the older Steeles Avenue units the slab has usually been patched a dozen times, and that all comes off before anything goes down.
Most requested in Milton: high-build epoxy with a polyaspartic topcoat in production and forklift aisles.
The 401 Business Park along Steeles Avenue, Market Drive and Nipissing Road is Milton's original industrial stock, built from the 1970s into the 1990s, which usually means a decent slab that has been sealed, patched and painted several times and never tested for moisture. Derry Green is the opposite problem: much of it was poured in the last three years, and green concrete with high slab moisture is the thing that kills a coating there.
In Milton's older plants the biggest line on the quote is usually preparation, not product. Forty years of shake-on hardeners, sealers and paint have to come off mechanically, and a quote that does not itemise that step is a quote that will grow. We list it separately so you can see exactly what you are paying for.
Every plant floor question comes back to the same three inputs: what gets spilled on it, how hot that spill is, and what rolls over it. We ask for the list first, then specify against the manufacturer's resistance chart for the exact system, which is the only place those answers actually live.
| System | Where it goes | Why it gets specified |
|---|---|---|
| Novolac epoxy | Acid handling, plating, battery rooms, chemical process bays | Published product data covers inorganic acids including 98% sulfuric, at 100% solids, with service to roughly 80°C. This is where standard bisphenol-A epoxy stops being the right answer. |
| Urethane cement mortar | Hot process, steam clean-down, foundry-adjacent, thermal cycling | Rated across roughly -40°F to 250°F with a 150°F-plus shock differential, and it moves at close to the same rate as the slab so it does not shear off under thermal cycling. |
| High-build epoxy with urethane topcoat | General production floors, assembly, packaging | The workhorse. Epoxy for build and adhesion, urethane or polyaspartic on top for abrasion, UV stability and faster return to service. |
| Static dissipative systems | Powder handling, solvent areas, electronics-adjacent lines | Where combustible dust or solvent vapour is in play, the floor becomes part of the grounding strategy rather than just a surface. |
| Machine plinth and base coving | Every equipment base, pit edge and pedestal | Coved up the plinth and sealed at the interface, so coolant and oil cannot get underneath the coating and lift it. |
A plant floor that has been running for twenty years has oil, coolant and hydraulic fluid driven down into the concrete. Grinding the surface alone does not solve that, it just exposes clean-looking concrete with contamination underneath waiting to reject the primer. Older stock needs degreasing, sometimes repeated, and a bond test before anything gets specified. This is the step most quotes skip and most failures come from.
Book a Site VisitThere is no such thing as a chemically resistant floor in general. There is a specific system with a specific resistance chart. Novolac extends the acid range, urethane handles solvent and thermal duty, standard epoxy has real limits. We ask what you run, then match the system and show you the data rather than promising broad resistance.
Read the GuidesWe work line by line and cell by cell, around fixed equipment and pits, on nights, weekends and shutdown windows. Fast-cure systems have equipment back on the floor within hours rather than days, and we coordinate with your millwrights on anything that has to be lifted or unbolted.
See PricingWe test the slab, write the scope and give you a fixed price. On a new building that includes the moisture reading nobody else takes, and you are not committing to anything by finding out.
Aggregate-filled mortars at a quarter inch and up are the answer where dropped tooling and heavy point loads are routine, not a thicker roll coat.
Machining floors get a system chosen for the coolant chemistry in use, with texture that still grips when the floor is oily.
Ovens, quench areas, wash bays and anywhere the floor swings temperature get urethane cement rather than epoxy.
A sealed, seamless floor keeps grinding dust and swarf sweepable instead of ground into the slab.
Walkways, hazard zones, forklift routes and equipment footprints marked into the system per ANSI Z535.1 colour convention.
ASTM C579 compressive results carry roughly 15% reproducibility variance, so we do not sell you on a small psi gap between two products.
Milton is the fastest-growing employment base we work in. The Town reports jobs up roughly a quarter since 2020 and close to two million square feet of new industrial space added in 2025 alone, most of it in Derry Green. That shapes the work: in the 401 Business Park we are usually stripping forty years of old sealers off a sound slab, and in Derry Green we are usually waiting on, or mitigating, a slab that is still giving off moisture. Both are routine. Neither should be guessed at.
We come out from Burlington, walk the floor with you, and take calcium chloride or in-situ RH readings on the same visit. On a new Derry Green slab this single test decides the system and the schedule.
Old sealers, hardeners and paint come off mechanically in the older units. New slabs are ground to open the surface and remove curing compound, which is the most common cause of a coating letting go on new construction.
We work in sections around receiving hours or a plant shutdown, then hand over data sheets, a maintenance sheet and a 5-year warranty on the installed system.
Twenty-seven Google reviews, a 5.0 average, and Christopher replies to every one of them personally. Milton is close enough to Burlington that the people who quote your floor are the people who install it.
"I had the pleasure of working with Surface Coating Experts, owned by Christopher, on a project in our condominium where one of the balconies and walkways required a complete repair."
What customers mention most: garage floor installation, epoxy quality, detailed work, and a smooth process from first quote to finished floor.
Every review gets a personal reply from the owner - the after-the-job care that keeps the rating a perfect 5.0.
This is not a sales call with a clipboard. Milton has two very different kinds of building and we price them differently: 401 Business Park units where the cost is in stripping what previous owners put down, and Derry Green buildings where the cost is in dealing honestly with a slab that is still curing. Both are workable. Both need testing first.
Free. No obligation. Usually within the week.
Prefer to talk it through? Call (905) 876-6957, Monday to Saturday, 6am to 6pm.
Tell us where the floor is and what runs on it. We will come out, test it and put a fixed price in writing.
Same service nearby: Manufacturing in Oakville · Manufacturing in Burlington
Milton is twenty minutes up Highway 25 from our base in Burlington, so the assessment itself is quick to arrange. What takes real time is a new slab that tests wet, which is common in Derry Green: either the concrete is given more time to dry, or a moisture mitigation primer goes down first and adds a day and a material cost. Testing early costs nothing and it means the date you pick is one we can actually hold.
Also see our industrial & commercial overview, epoxy flooring in Milton and published pricing.
Tell us the square footage, what runs on the floor and whether the building is new or one of the original Steeles Avenue units. On new Milton slabs we test moisture before anything else, because that is what decides the system.
Free, no obligation, and you keep the written scope whether you use us or not.