Static dissipative and conductive floor systems for Milton electronics manufacturers, PCB and assembly operations, data centres and battery facilities. Grounded, installed as a system and resistance tested on handover.
Free on-site assessment, usually within the week. Milton is a short drive from our Burlington base. Written scope, fixed price, no obligation.
This is the one category where the damage is usually invisible, which is exactly why it goes unfixed for years.
Electrostatic damage is frequently latent. The part passes test, fails in the field, and the warranty claim never gets connected to the floor it was assembled on.
If the floor was never tested to ANSI/ESD S7.1 and you hold no resistance results, your compliance verification plan has a hole in it that an auditor will find before you do.
A dissipative coating with no grounding grid and no earth points measures nothing useful. A lot of facilities are paying for an ESD floor they do not actually have.
Bare slab under a raised access floor sheds continuously into equipment that is spending energy filtering it back out.
Milton's electrical and controls operations are mostly in newer buildings, which makes the grounding easier to get right and the slab easier to get wrong. A dissipative floor over a wet slab fails like any other, and the earth path only works if it was designed in before the primer.
The floor is a small number next to one field failure you cannot explain.
Eaton and Schneider Electric are both named by InvestMilton in the town's business parks, and the Town reports professional, scientific and technical services employment up more than a third since 2021. That is not yet the electronics cluster Burlington has, but it is a real base of electrical, controls and test operations that need a static-dissipative floor with a reliable earth path. Because so much of Milton's stock is new, the good news is that the grounding is usually designed in before the primer goes down rather than retrofitted into a building with forty years of electrical modifications.
Most requested in Milton: static-dissipative epoxy with grounding designed into new construction.
The 401 Business Park along Steeles Avenue, Market Drive and Nipissing Road is Milton's original industrial stock, built from the 1970s into the 1990s, which usually means a decent slab that has been sealed, patched and painted several times and never tested for moisture. Derry Green is the opposite problem: much of it was poured in the last three years, and green concrete with high slab moisture is the thing that kills a coating there.
Most of the Milton ESD work we quote is in a building new enough that the grounding can be designed properly from the start. We still ask for a qualified electrical engineer to specify the earth linkage, because that is the part of an ESD floor that a coating contractor should not be improvising.
ANSI/ESD S20.20 does not care what the coating tin says. It asks for a flooring and footwear system measuring under 1.0 x 10⁹ ohms and a peak body voltage under 100 V. Both. A dissipative coating installed without a grounding grid meets neither, and that is the most common ESD floor failure we get called in to fix.
| System | Where it goes | Why it gets specified |
|---|---|---|
| Static dissipative epoxy | EPA workstations, assembly, PCB handling, test areas | Dissipative sits above 1.0 x 10⁶ and below 1.0 x 10⁹ ohms resistance to ground. Typically 2 to 3 mm, foot traffic at 24 hours, heavy traffic at 48, full cure at 7 days. |
| Conductive epoxy | Higher risk areas, explosives-adjacent, some battery work | Conductive is 1.0 x 10⁶ ohms and below. A lower resistance is not automatically better, it is a different design decision, and it has electrical safety implications. |
| Copper grounding grid and earth points | Underneath the whole system | Copper tape bridging joints, tied to earth points installed with redundancy. Manufacturer guidance calls for a minimum of two earth points per floor area so a single failure does not orphan the floor. |
| Standard high-build epoxy | Data centre halls, corridors, non-EPA areas | Not everything needs to be ESD. Sealing bare slab under and around a raised access floor kills dust without paying for a grounded system where you do not need one. |
| Handover resistance testing | Every ESD install | Point-to-point and point-to-groundable-point testing per ANSI/ESD S7.1, with results documented for your compliance verification plan. |
The floor is one element in a grounded path. We install a conductive primer, lay copper tape bridging the joints, tie into earth points placed with redundancy, and have the earth linkage cabling specified by a qualified electrical engineer rather than guessed at. A dissipative coating rolled over bare concrete with no grid is not an ESD floor, whatever the data sheet says.
Book a Site VisitANSI/ESD S7.1 characterises floor material resistance point-to-point and point-to-groundable-point, both under 1.0 x 10⁹ ohms for S20.20. We test at completion and hand you the results. S20.20 also requires a compliance verification plan with periodic retesting, and the interval is set by your facility rather than by the standard, so we will not invent one for you.
Read the GuidesWe do not sell ESD S20.20 certified floors, because S20.20 certifies a facility's ESD control programme, not a coating and not a contractor. What we install is a floor that can be qualified within your programme, tested and documented. We also avoid the word anti-static: it is not a standardised term, it usually just means reduced tribocharging, and it has no verified resistance range or ground path behind it.
See PricingWe test the slab, write the scope and give you a fixed price. On a new building that includes the moisture reading nobody else takes, and you are not committing to anything by finding out.
Conductive is 1.0 x 10⁶ ohms and below. Dissipative is above 1.0 x 10⁶ and below 1.0 x 10⁹. Test method is ASTM F150 and ANSI/ESD S7.1.
S20.20 requires peak body voltage under 100 V per ANSI/ESD STM97.2, measured with the footwear in use. Resistance alone is not compliance.
In a data centre the coated slab often sits under a raised floor whose stringers and pedestals carry their own grounding. We coordinate rather than assume.
Sealing bare concrete beneath a raised access floor is one of the highest value, lowest cost jobs in a data hall.
Loaded server carts are harder on a floor than anything else in the building, so abrasion resistance drives the topcoat choice.
We work to the spec your programme sets. If you do not have one yet, we will tell you that the floor is only one element of it.
Milton is the fastest-growing employment base we work in. The Town reports jobs up roughly a quarter since 2020 and close to two million square feet of new industrial space added in 2025 alone, most of it in Derry Green. That shapes the work: in the 401 Business Park we are usually stripping forty years of old sealers off a sound slab, and in Derry Green we are usually waiting on, or mitigating, a slab that is still giving off moisture. Both are routine. Neither should be guessed at.
We come out from Burlington, walk the floor with you, and take calcium chloride or in-situ RH readings on the same visit. On a new Derry Green slab this single test decides the system and the schedule.
Old sealers, hardeners and paint come off mechanically in the older units. New slabs are ground to open the surface and remove curing compound, which is the most common cause of a coating letting go on new construction.
We work in sections around receiving hours or a plant shutdown, then hand over data sheets, a maintenance sheet and a 5-year warranty on the installed system.
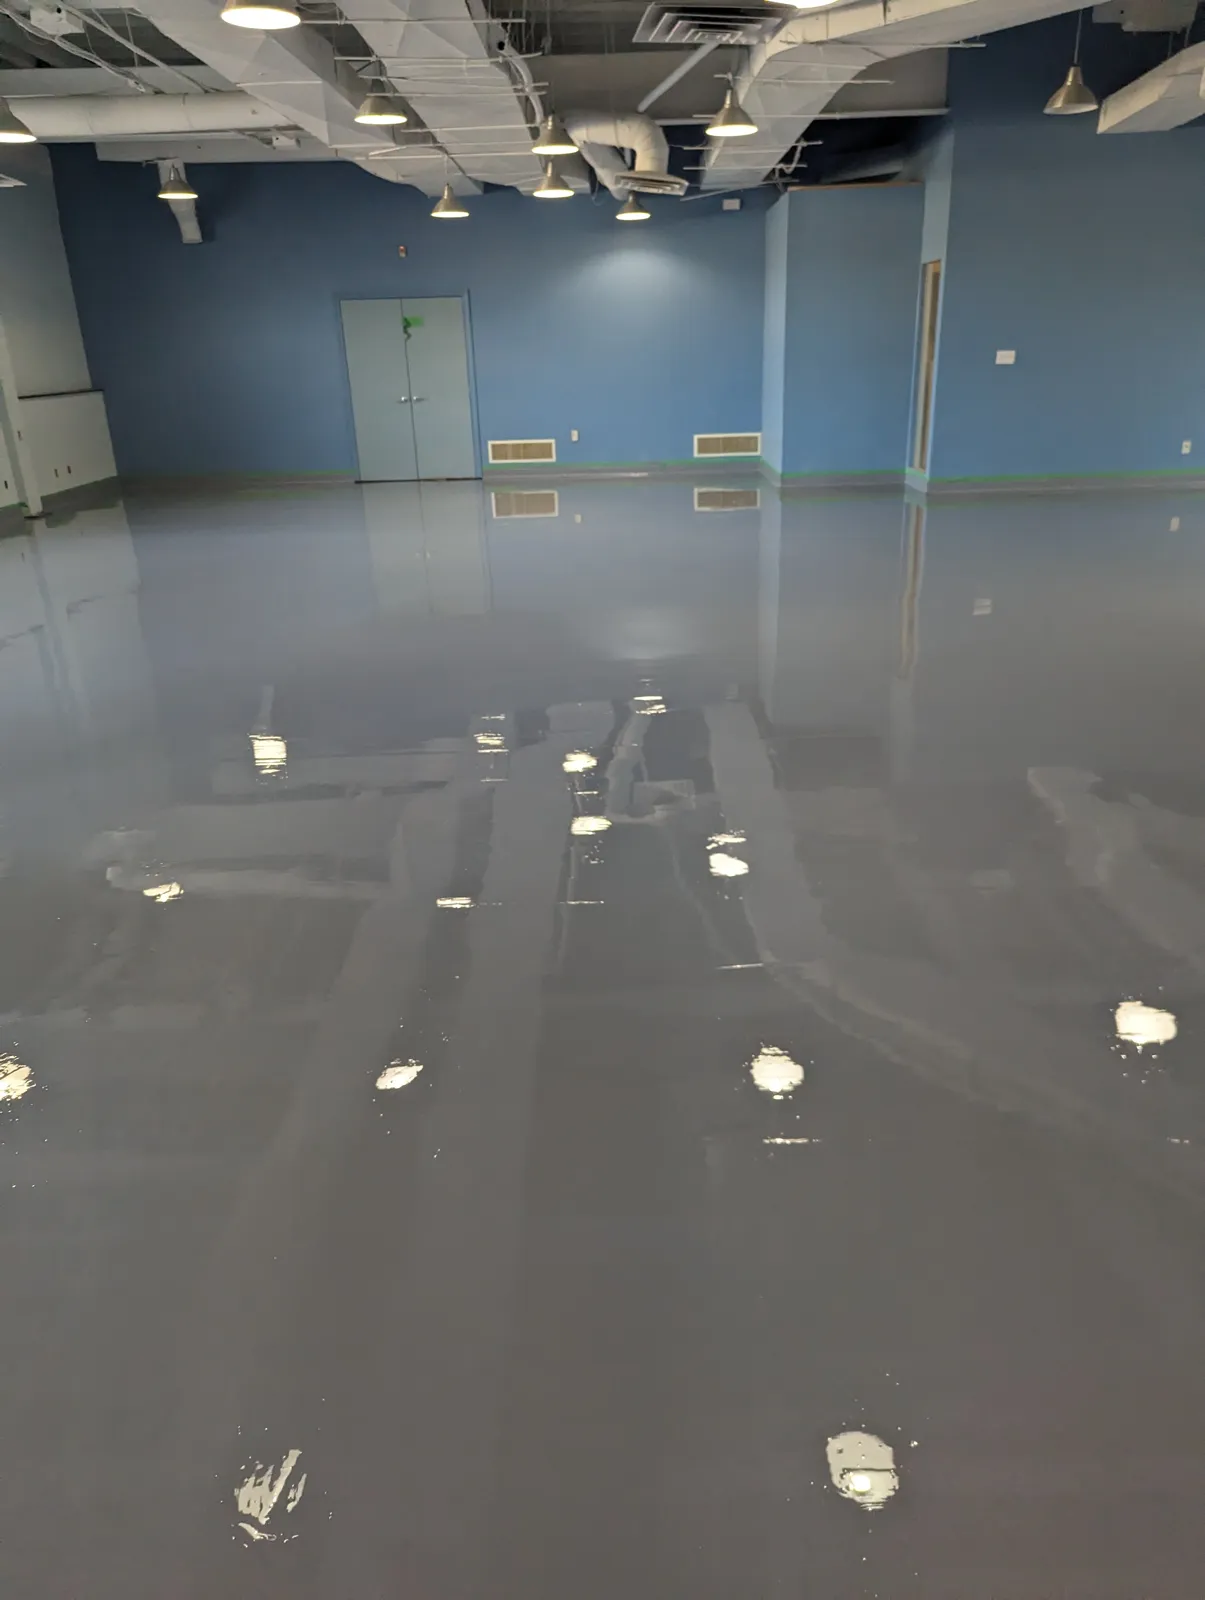
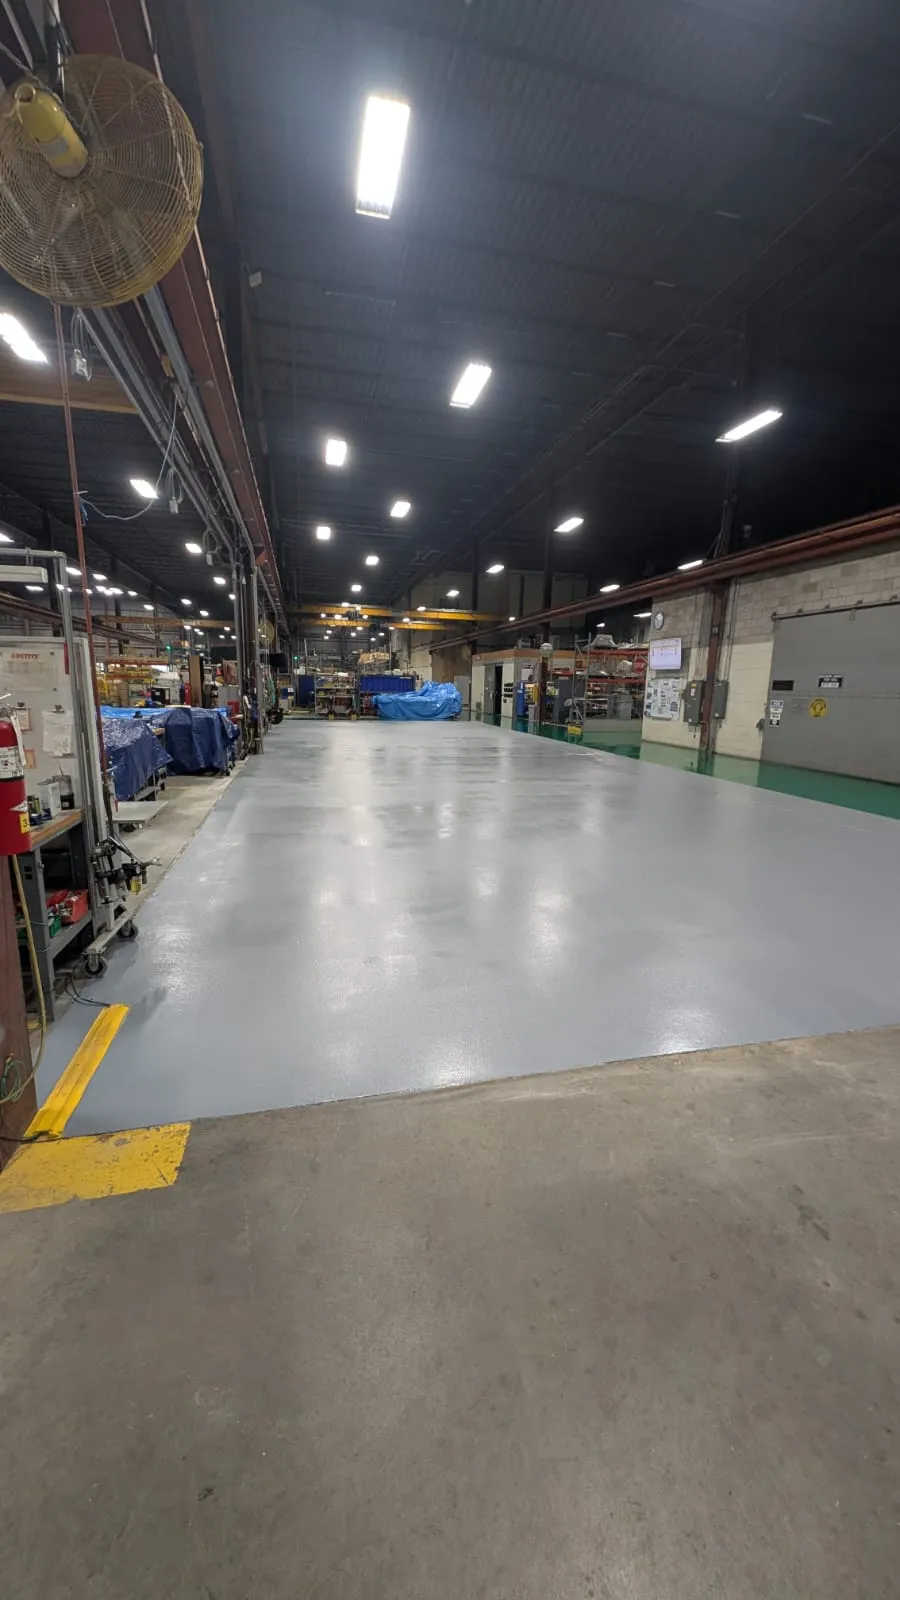
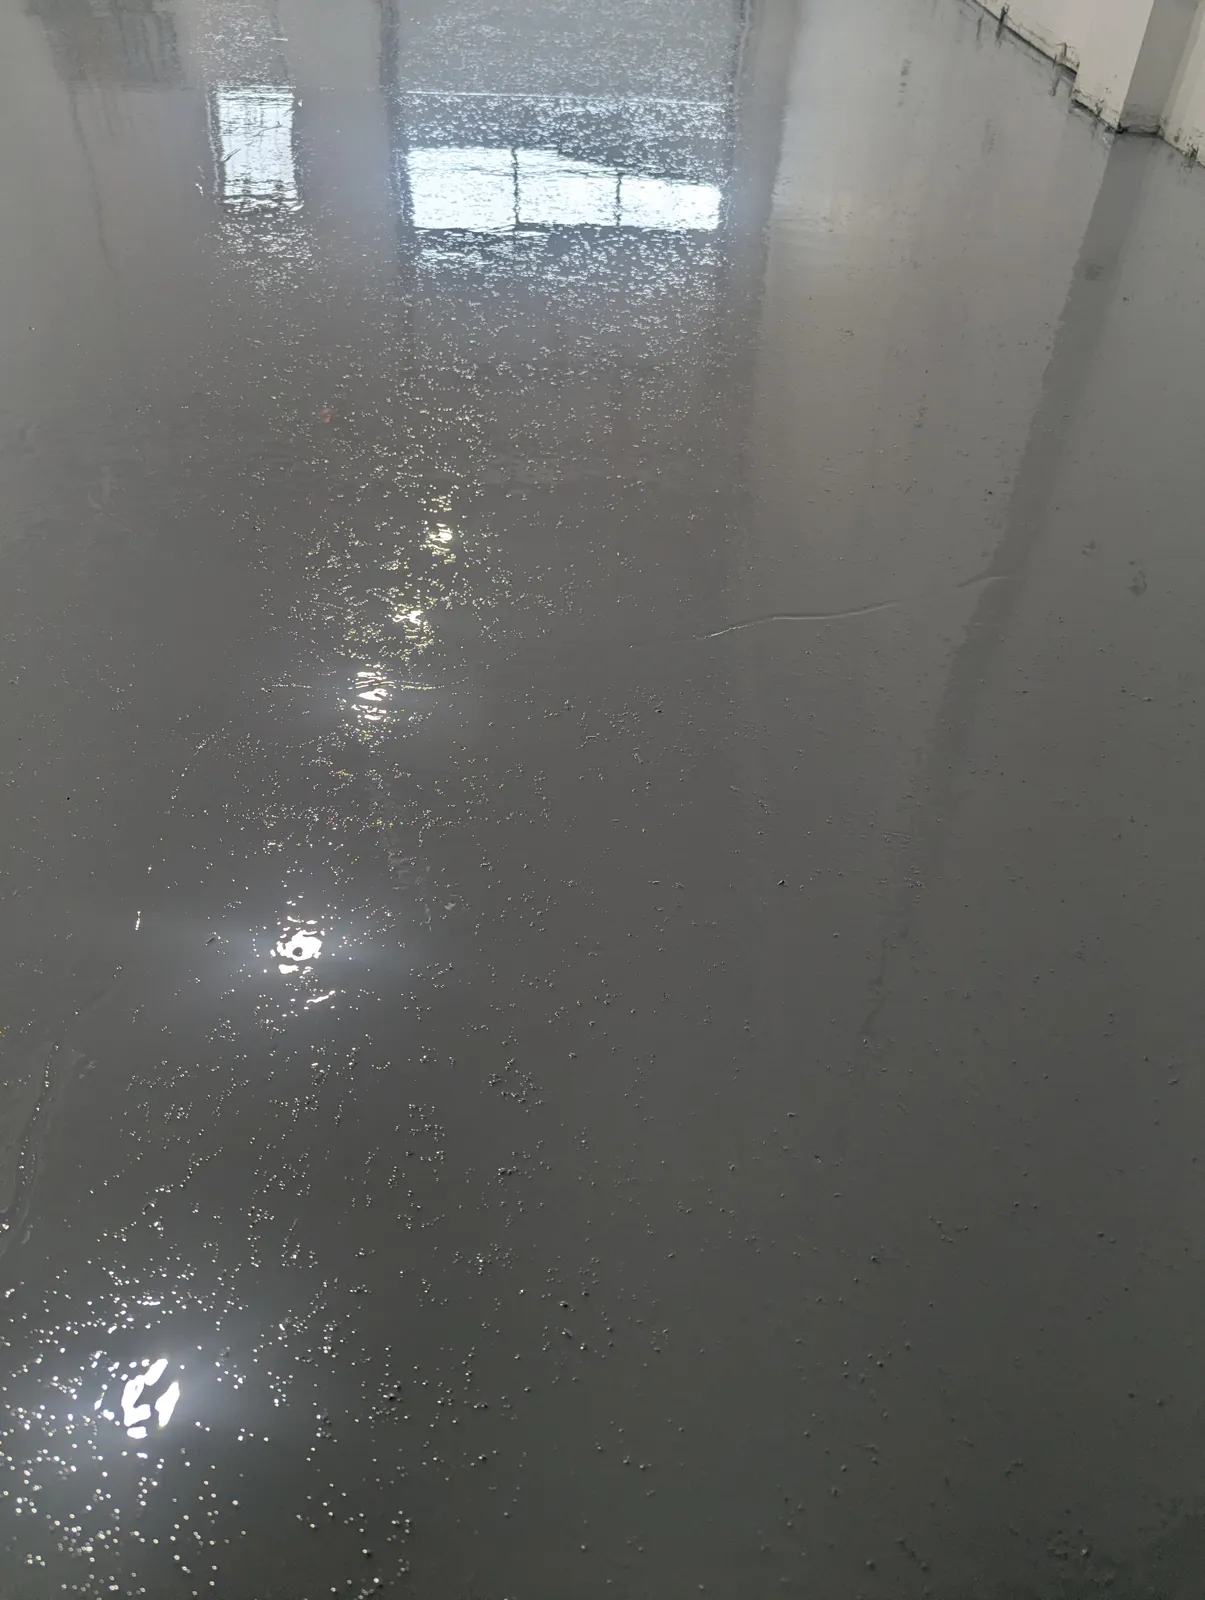
Twenty-seven Google reviews, a 5.0 average, and Christopher replies to every one of them personally. Milton is close enough to Burlington that the people who quote your floor are the people who install it.
"I had the pleasure of working with Surface Coating Experts, owned by Christopher, on a project in our condominium where one of the balconies and walkways required a complete repair."
What customers mention most: garage floor installation, epoxy quality, detailed work, and a smooth process from first quote to finished floor.
Every review gets a personal reply from the owner - the after-the-job care that keeps the rating a perfect 5.0.
This is not a sales call with a clipboard. Milton has two very different kinds of building and we price them differently: 401 Business Park units where the cost is in stripping what previous owners put down, and Derry Green buildings where the cost is in dealing honestly with a slab that is still curing. Both are workable. Both need testing first.
Free. No obligation. Usually within the week.
Prefer to talk it through? Call (905) 876-6957, Monday to Saturday, 6am to 6pm.
Tell us where the floor is and what runs on it. We will come out, test it and put a fixed price in writing.
Same service nearby: Electronics & ESD in Oakville · Electronics & ESD in Burlington
Milton is twenty minutes up Highway 25 from our base in Burlington, so the assessment itself is quick to arrange. What takes real time is a new slab that tests wet, which is common in Derry Green: either the concrete is given more time to dry, or a moisture mitigation primer goes down first and adds a day and a material cost. Testing early costs nothing and it means the date you pick is one we can actually hold.
Also see our industrial & commercial overview, epoxy flooring in Milton and published pricing.
Tell us the square footage, what runs on the floor and whether the building is new or one of the original Steeles Avenue units. On new Milton slabs we test moisture before anything else, because that is what decides the system.
Free, no obligation, and you keep the written scope whether you use us or not.